Explore our CE-certified structural steel shelving systems designed to maximize cubic storage volume and withstand the demanding throughput of global distribution hubs.
A global leader in structural rack fabrication, robotic handling system design, and turn-key warehouse engineering since 2015.
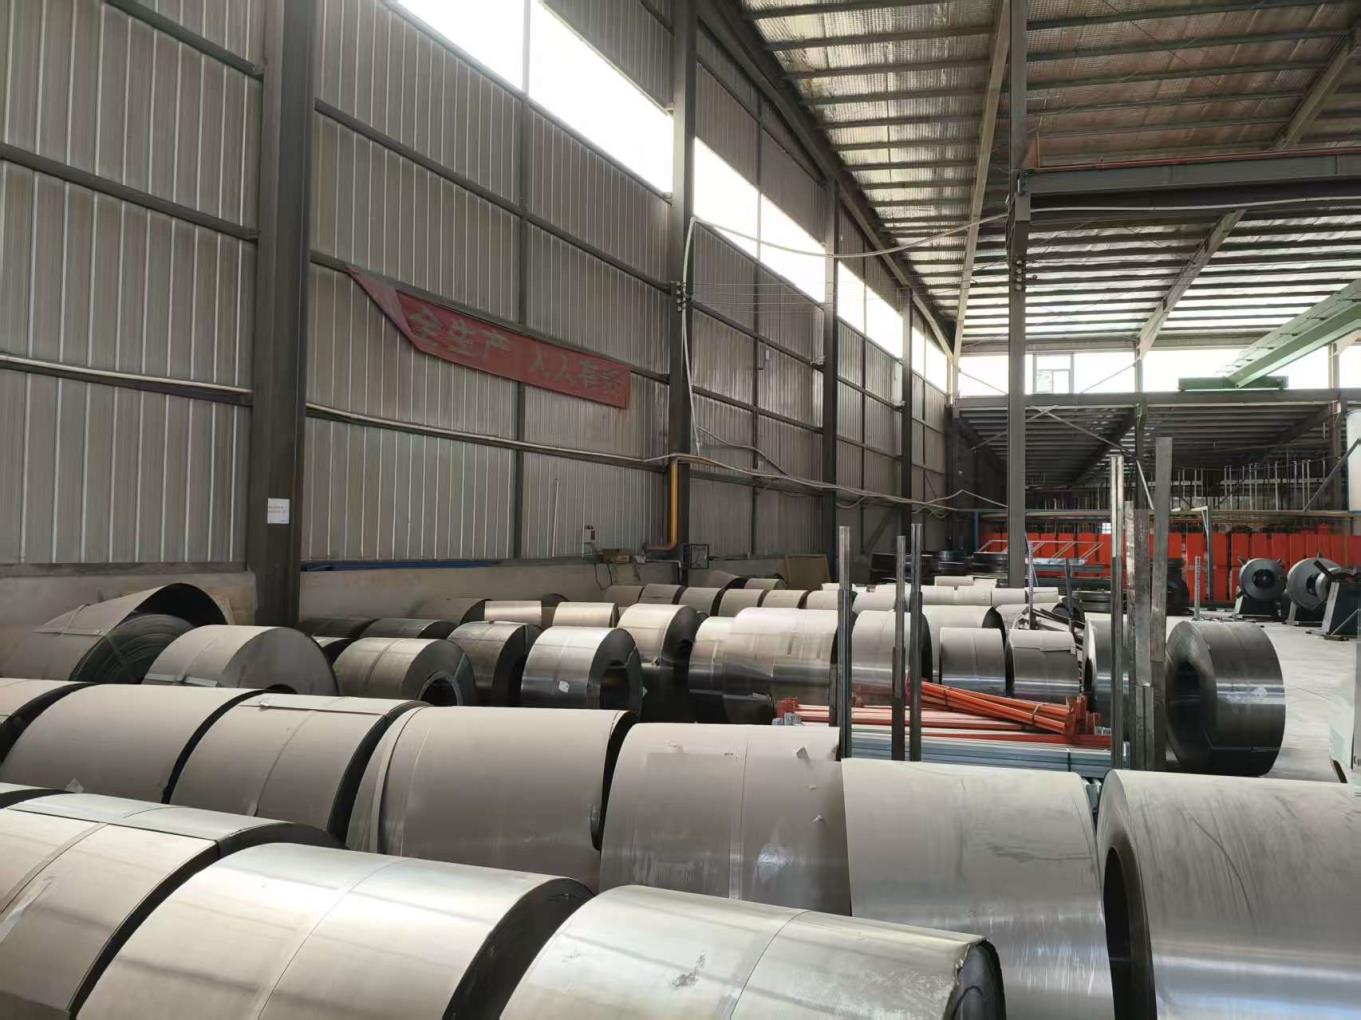
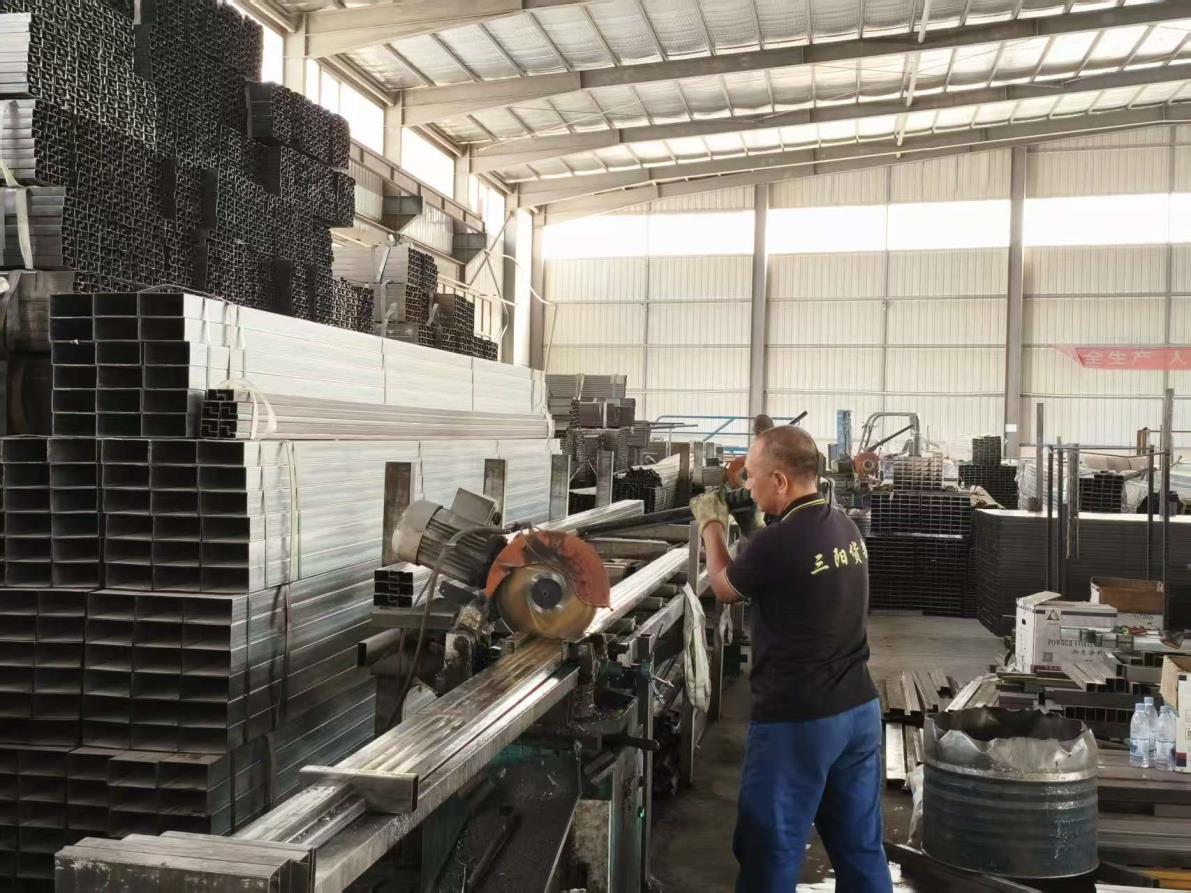
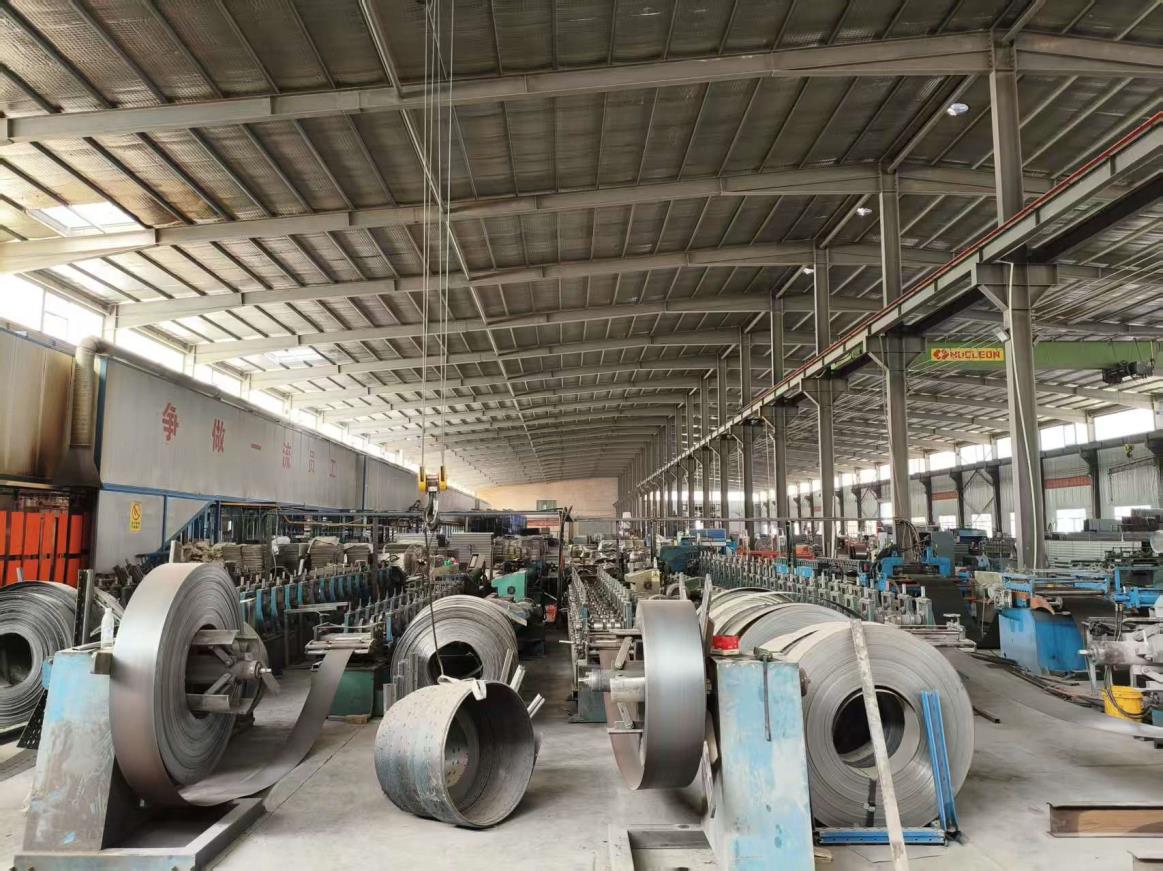
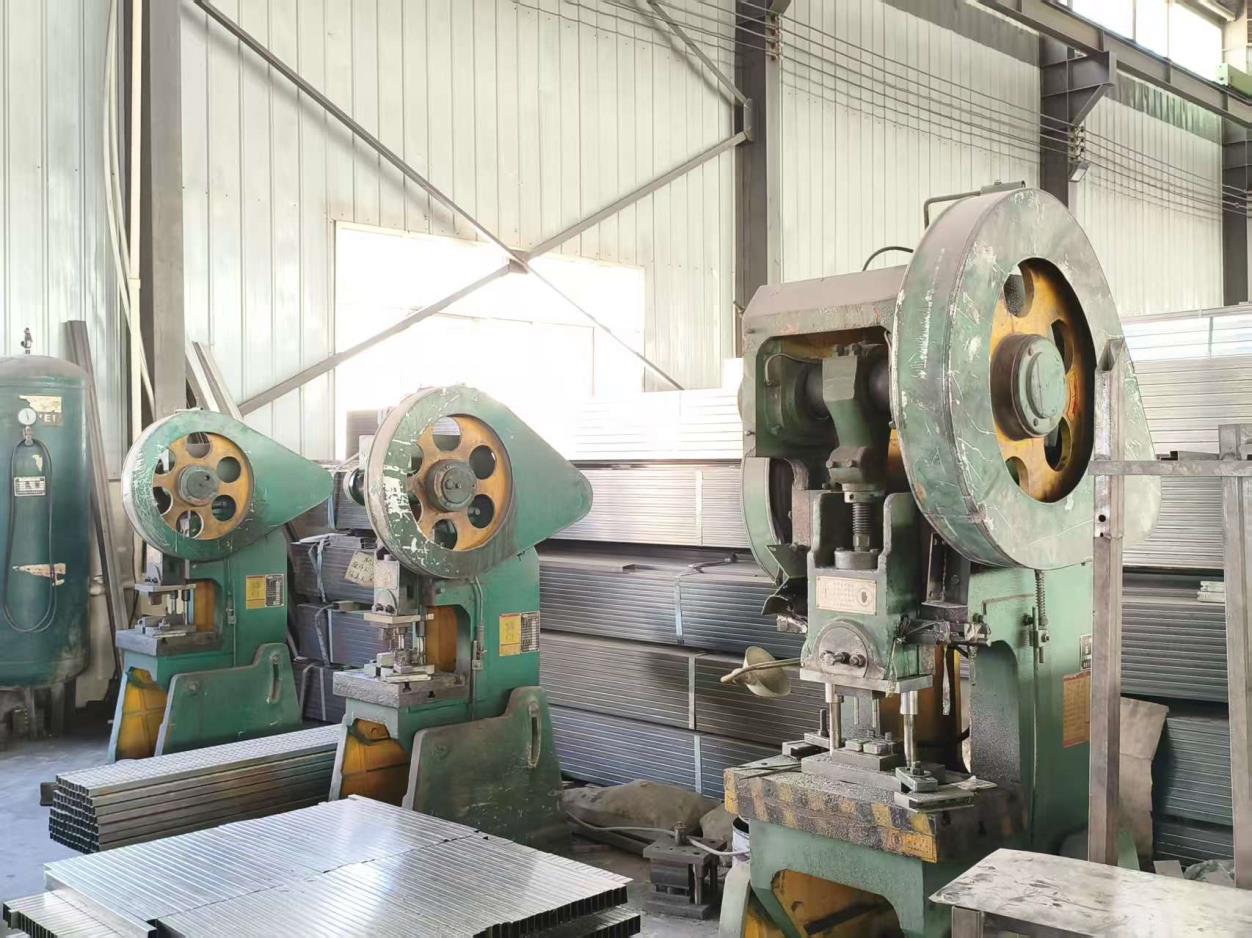
Established in 2015, Shenzhen Sanyang Storage Equipment Manufacturing Co., Ltd. is a leading manufacturer specializing in heavy-duty industrial pallet racking, warehouse shelving systems, and automated material handling solutions. Located in Shenzhen, our modern facility spans a total building area of 38,000 m², equipped with advanced automated roll-forming machines, laser cutters, and robot welding lines.
With over 12 years of industry experience and 8 years of active export experience, Sanyang has expanded its international footprint, achieving an annual export revenue of $28 million USD. Our main overseas markets cover North America, Western Europe, Southeast Asia, and the Middle East, primarily serving global logistics hubs, e-commerce fulfillment centers, third-party logistics (3PL) providers, and large manufacturing enterprises.
Quality and precision are at the core of our operations. Supported by 35 full-time QC inspectors, we implement rigorous quality assurance protocols using ultrasonic weld flaw detection, coating thickness testing, and heavy-load stress tests to ensure strict compliance with ISO9001 and international FEM/ANSI safety standards. Backed by a strong OEM/ODM background and a robust network of 1,200 supply chain partners, we offer highly customizable options—ranging from custom dimensions and load capacities to specialized powder coatings and seismic-resistant structural designs.
Innovation drives our continuous growth. Our team of 18 R&D engineers focuses on developing high-density and automated storage systems, successfully launching 65 new products last year alone. Sanyang remains dedicated to providing safe, space-saving, and cost-effective storage solutions for our global clientele.
Analyzing supply chain pressures, automated handling shifts, and structural integrity requirements reshaping international warehousing.
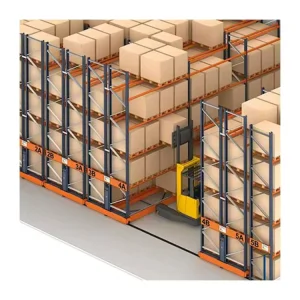
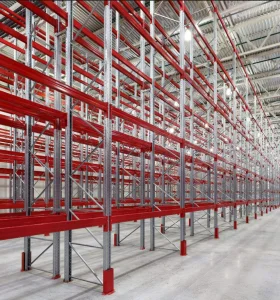
Industrial storage real estate prices have grown exponentially across the globe. Modern enterprises can no longer expand horizontally; instead, vertical space optimization through multi-tier mezzanines, narrow-aisle selective racking, and mobile vertical shelving units represents the industry standard for optimizing floor-to-ceiling volume.
CE Certification across the European Economic Area demands strict conformity to EN 15512, EN 15620, and EN 15635 structural calculation protocols. Certified factories guarantee steel yield strength, load deflection boundaries, and reliable weld penetration, mitigating structural collapse risks under severe seismic or load stress conditions.
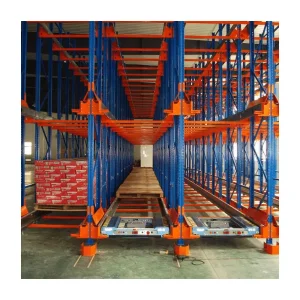
Static storage has rapidly evolved into high-throughput ecosystems. Automated Storage and Retrieval Systems (ASRS), four-way radio pallet shuttles, and electric mobile shelving demand tight dimensional tolerances of ±0.5mm, requiring precision manufacturing setups that eliminate operational friction for automated machinery.
Combining world-class steel processing efficiency with comprehensive automated manufacturing workflows to deliver high-quality, cost-competitive warehouse platforms.
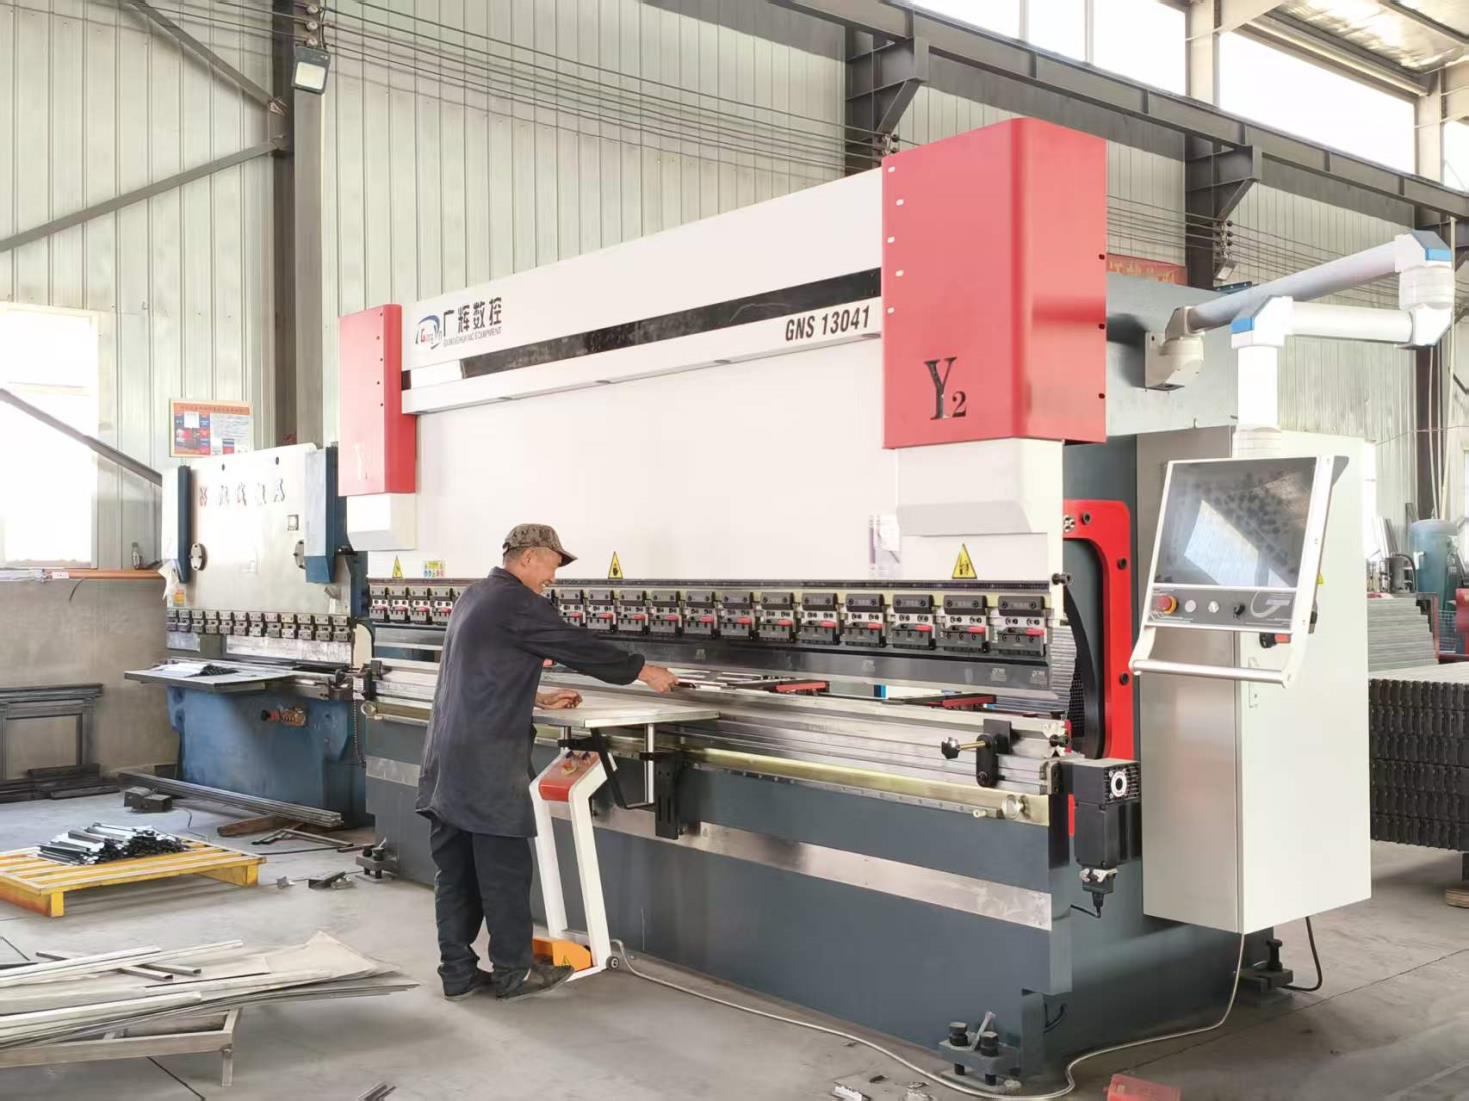
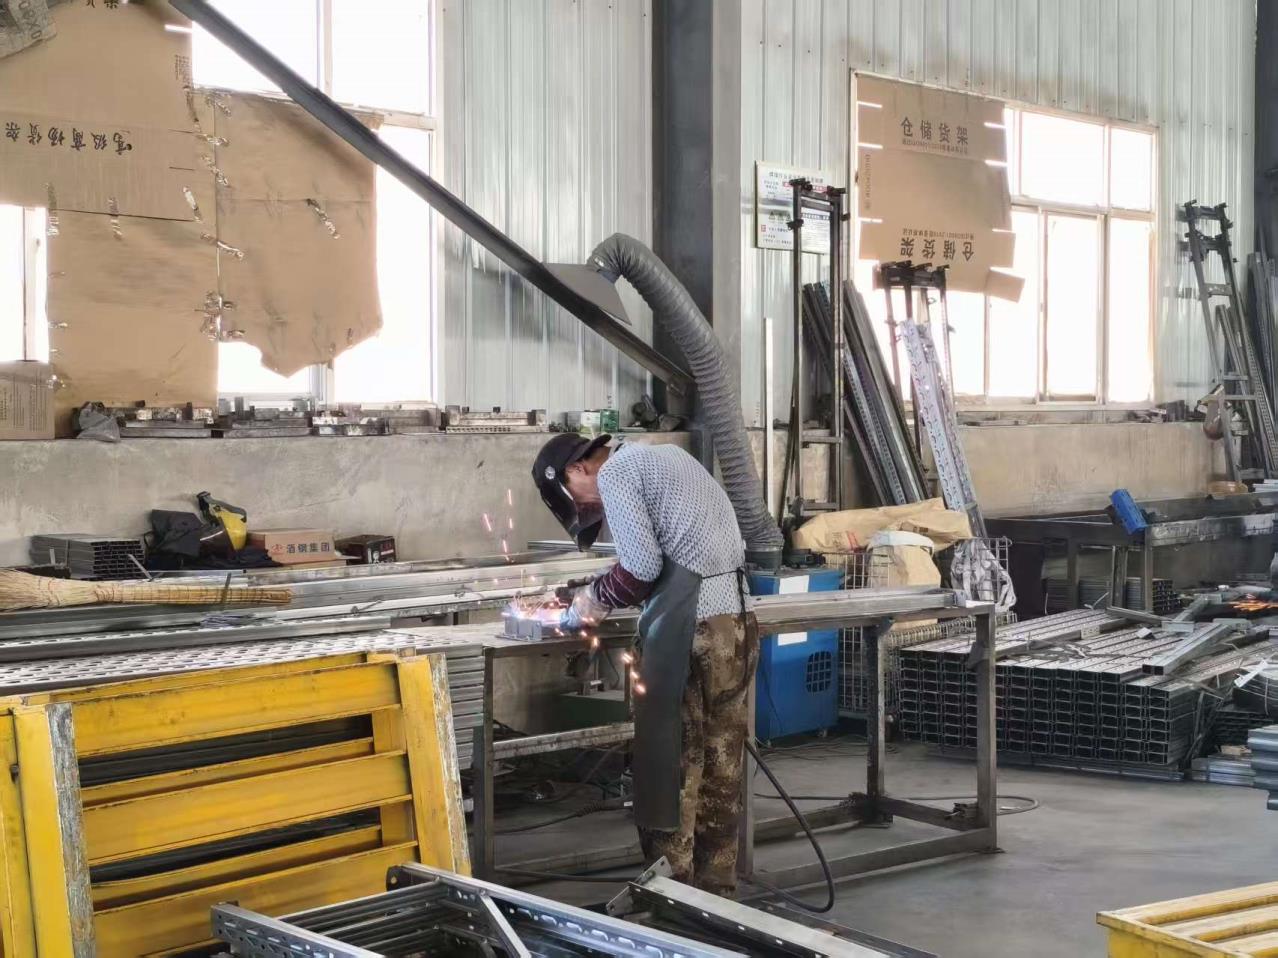
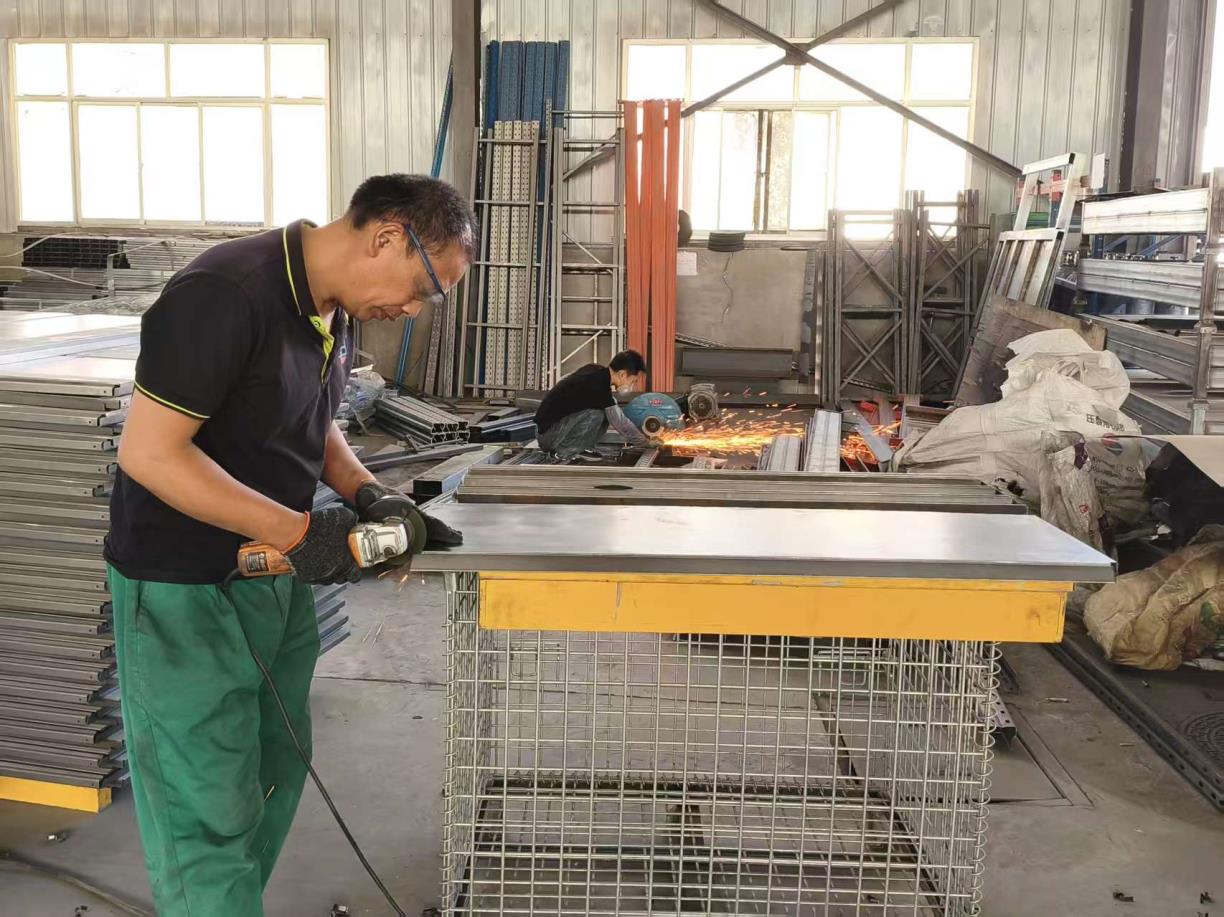
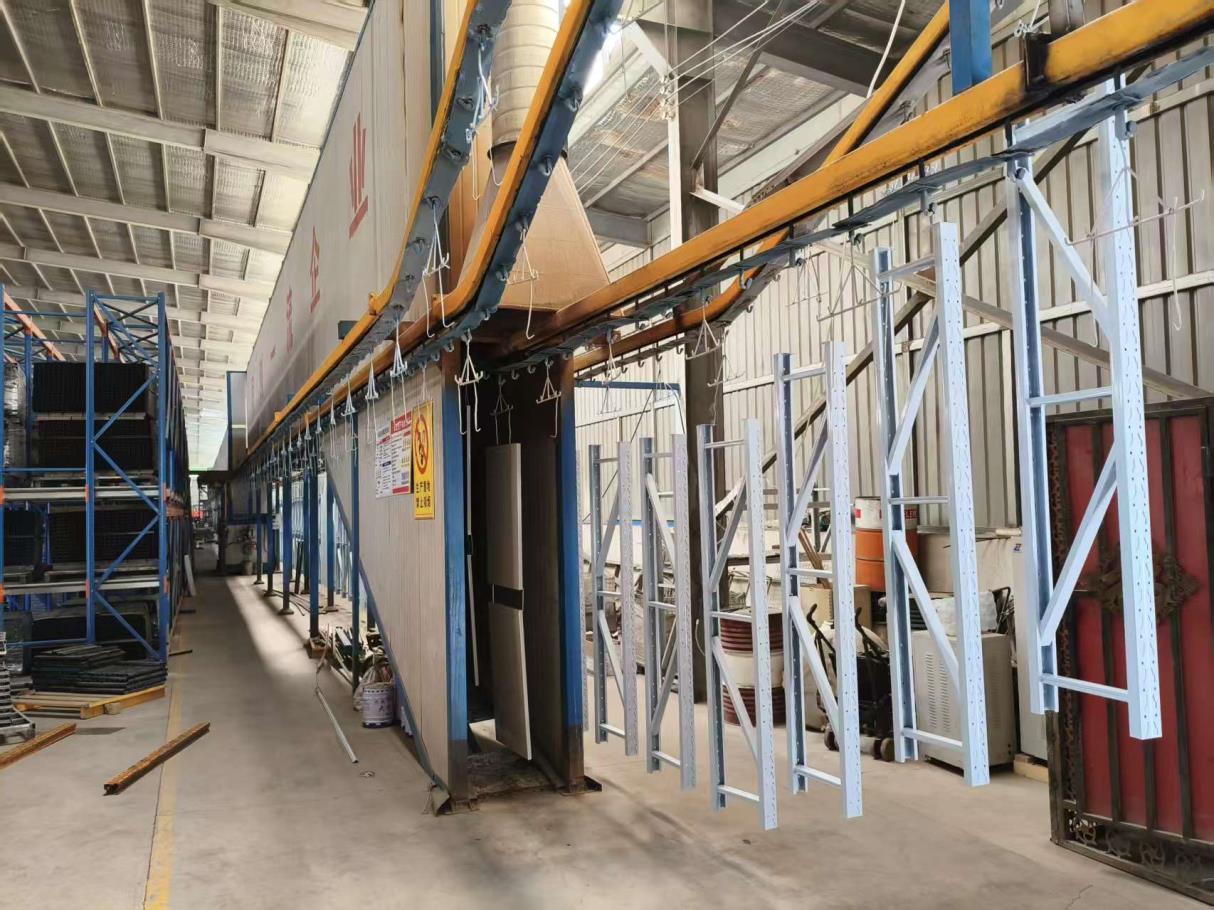
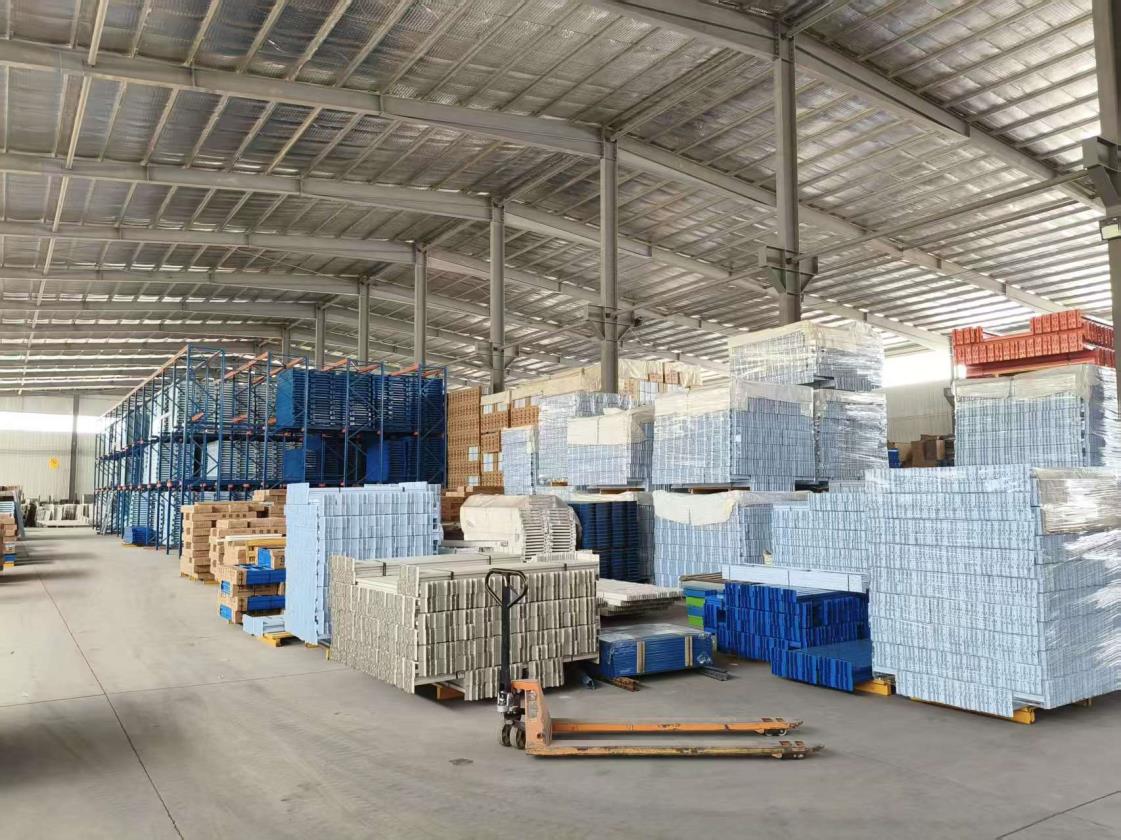
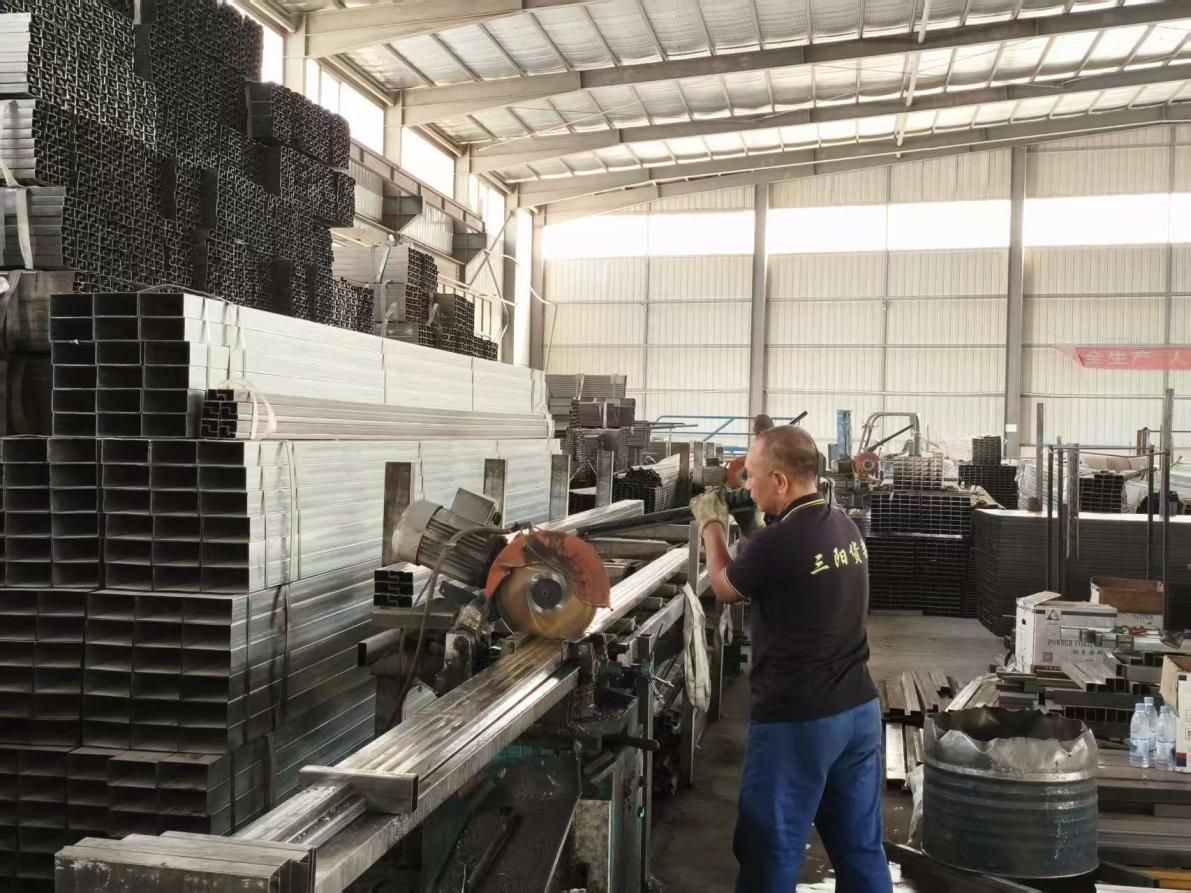
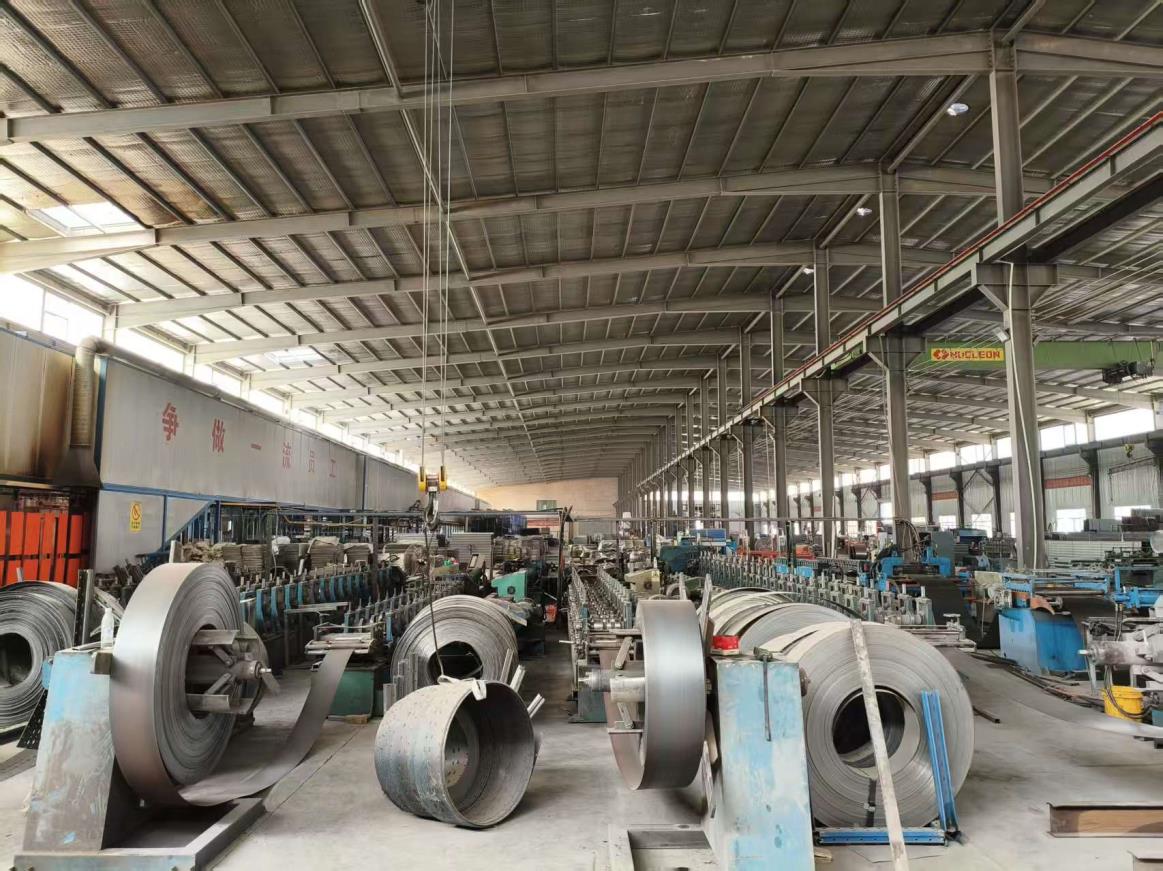
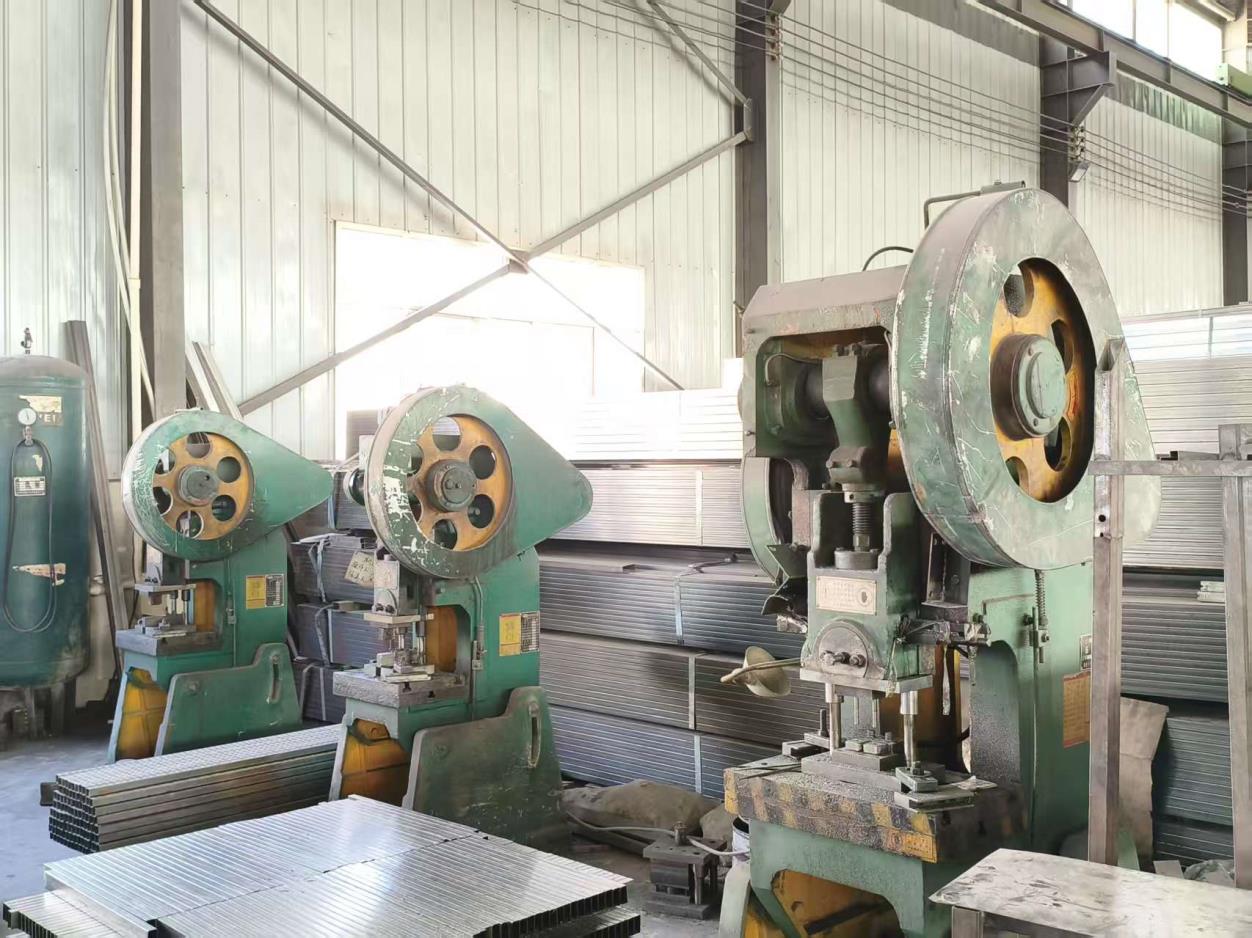
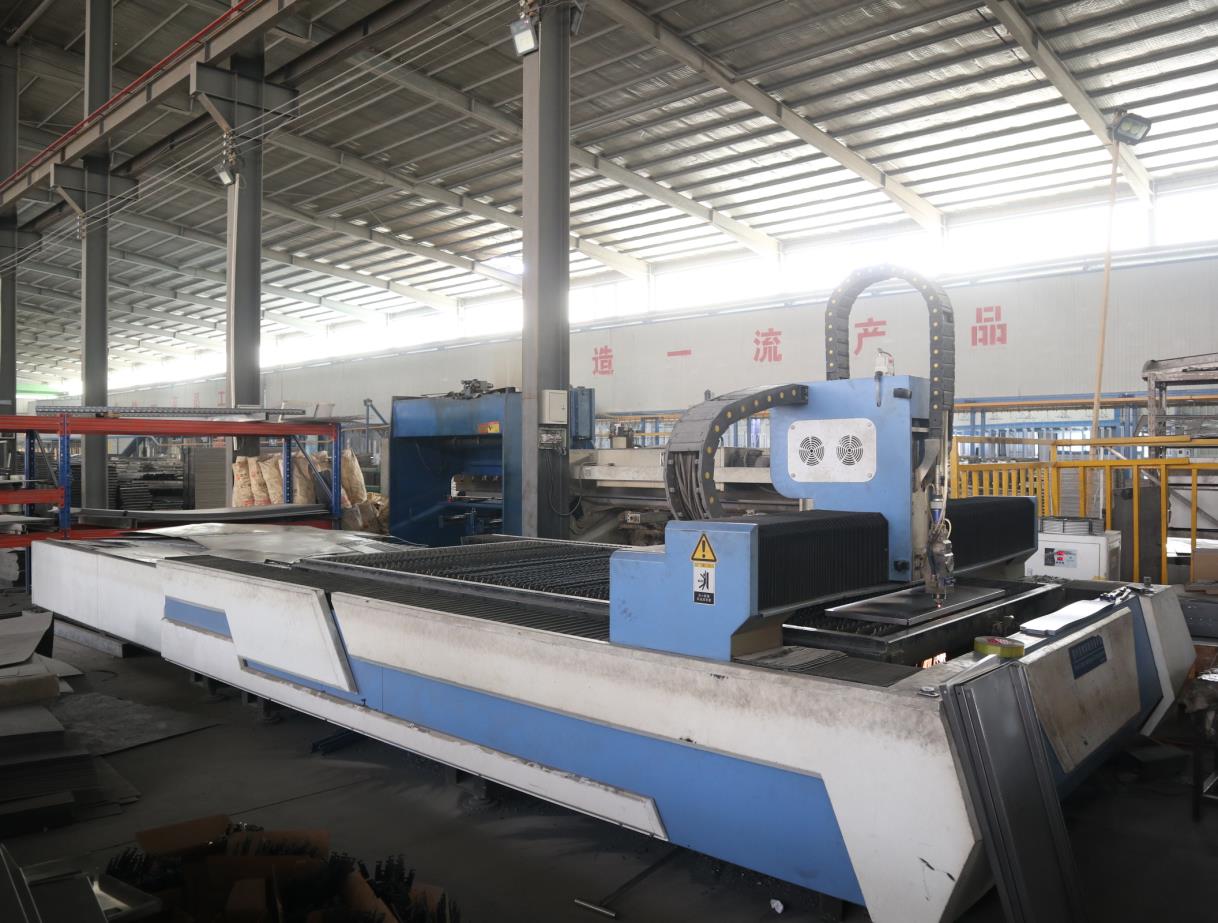
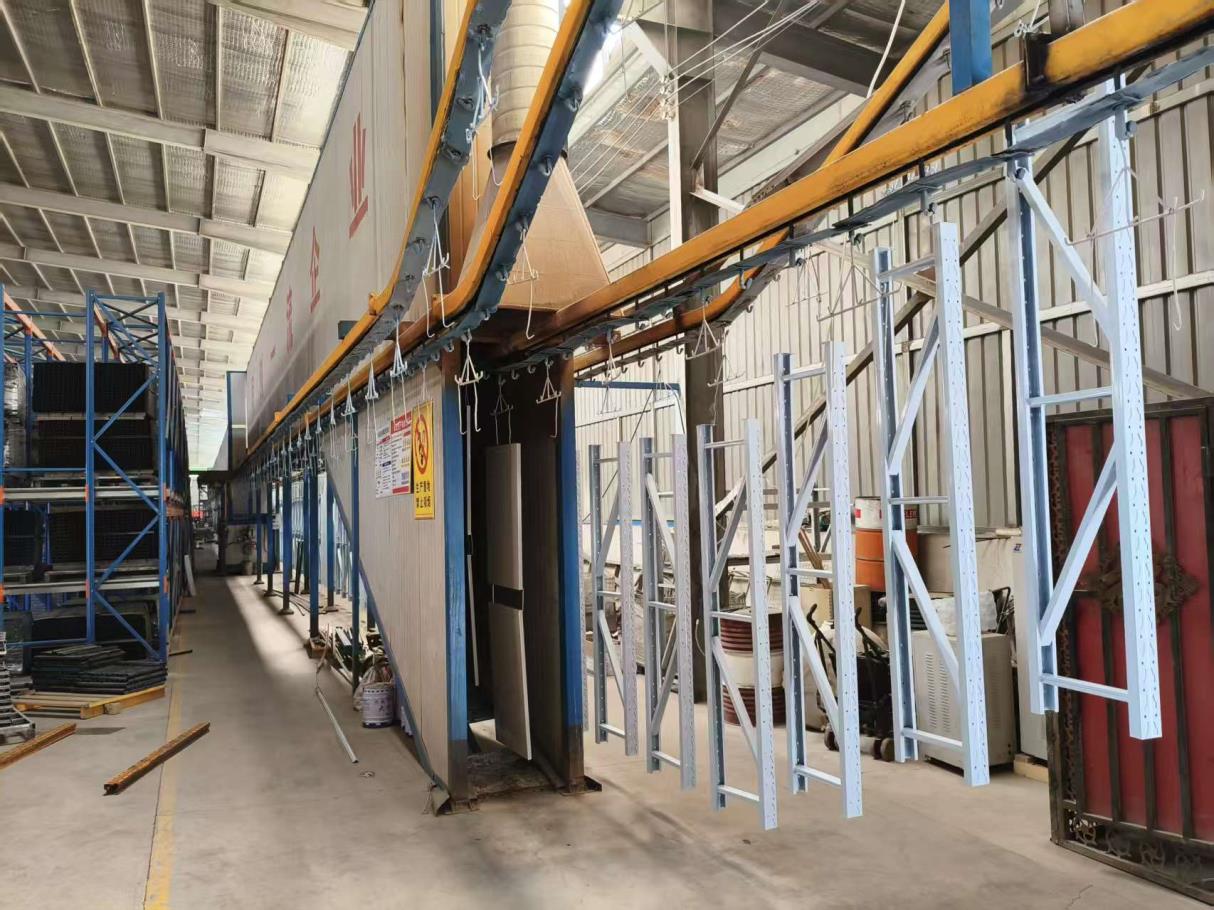
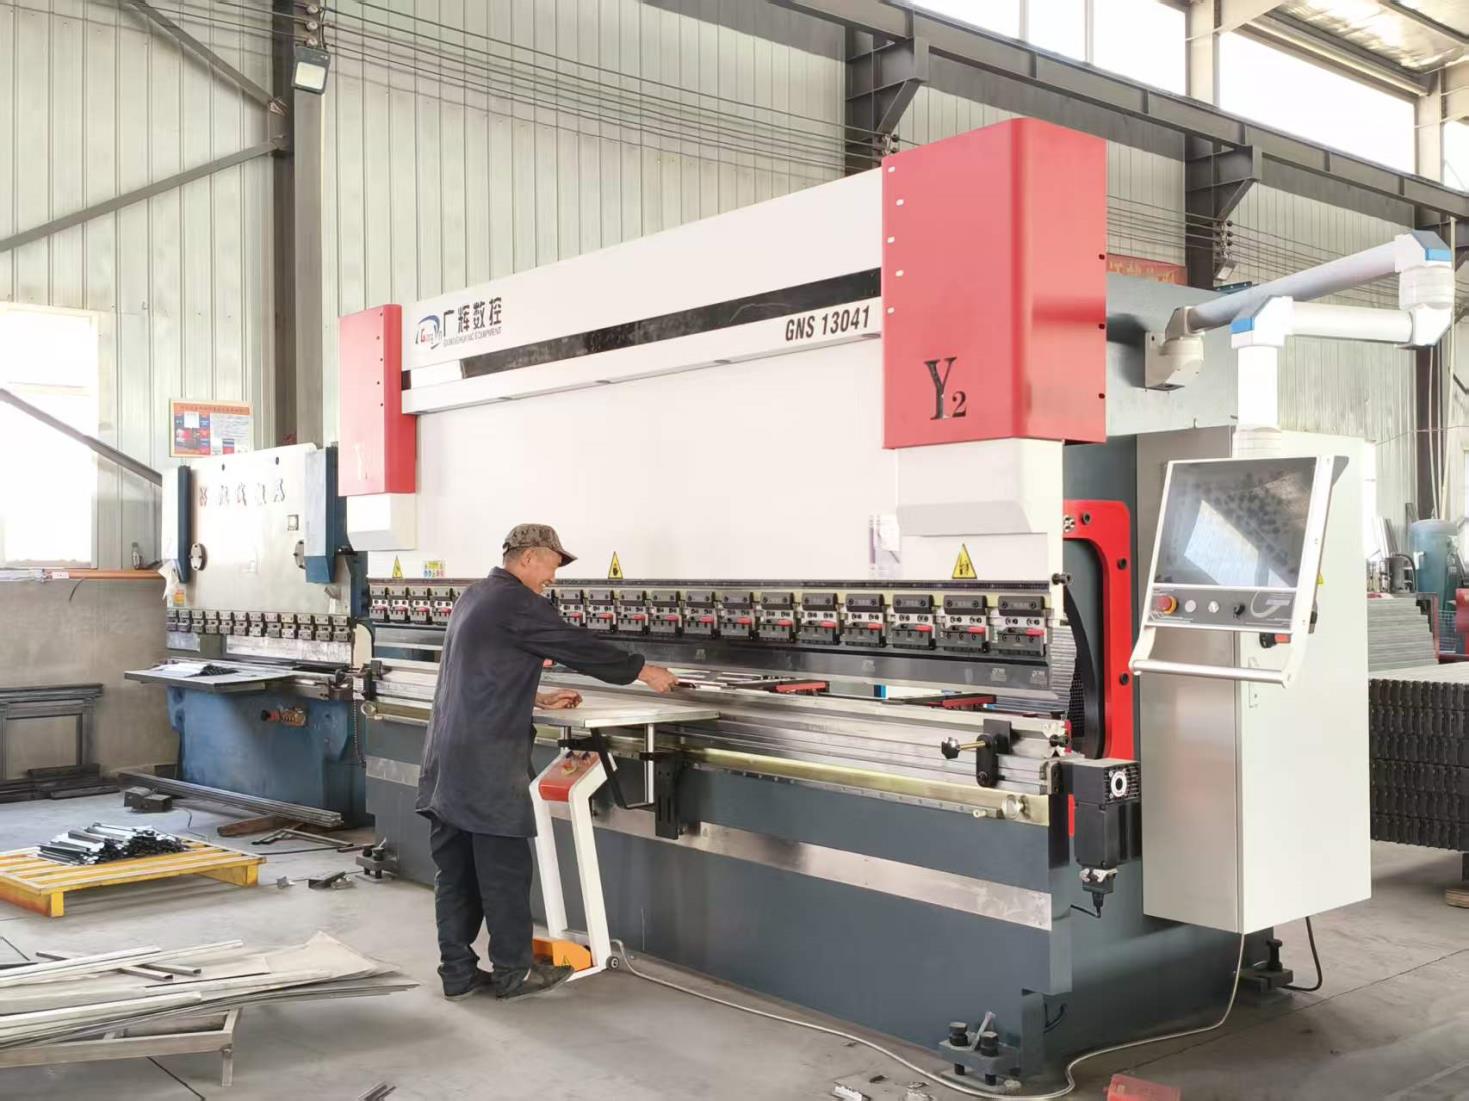
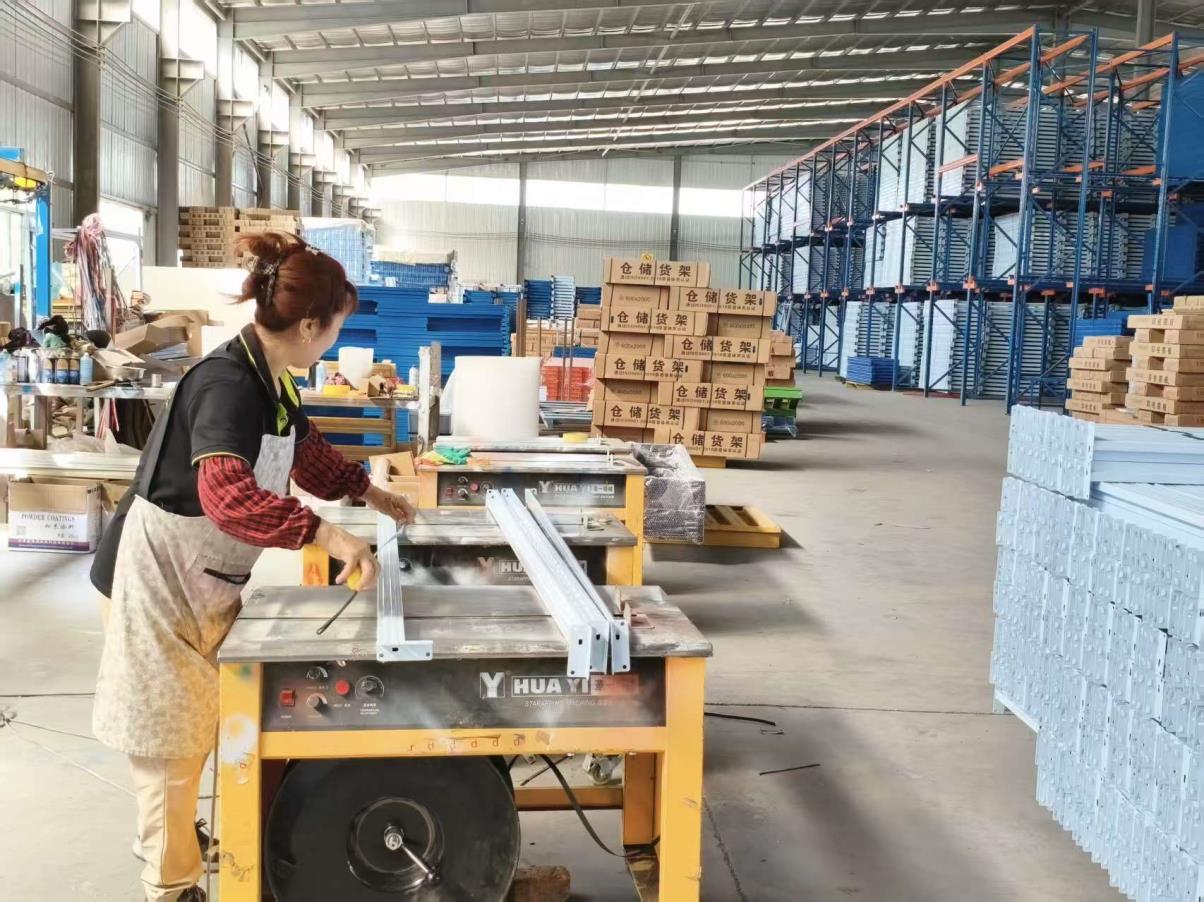
Custom structural engineering tailored to operational parameters, material properties, and vertical density constraints.
Refrigerated warehouse space incurs extremely high utility costs. Utilizing dense drive-in racks and radio shuttle systems minimizes chilled cubic volume, while low-temperature epoxy powder coatings prevent steel embrittlement down to -30°C.
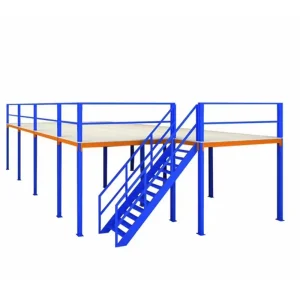
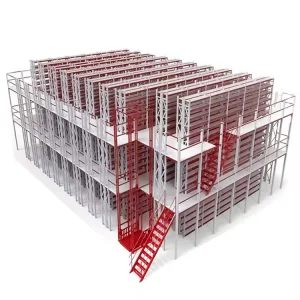
Demanding multi-tier mezzanine floors and modular boltless shelving with integrated pick towers allow hundreds of operatives to simultaneously execute split-case picking, maximizing SKU capacity across vertical tiers.
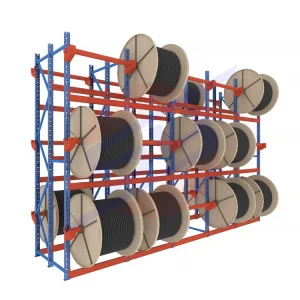
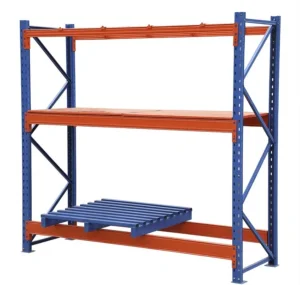
Structural cantilever racks and heavy-duty selective steel racking provide engineered support for unpalletized extrusions, steel piping, machinery parts, and automotive dies with individual section capacities exceeding 5,000kg.
Essential structural and compliance questions answered by our chief structural engineering specialists.
Under European standards (EN 15512, EN 15620, EN 15635), CE-certified industrial racking mandates certified raw material traceability (e.g., Q235B, Q355B structural steel), documented finite element analysis (FEA) for dynamic loads, strict deflection limits under maximum rated loads (typically L/200), and comprehensive non-destructive testing on critical welds.
Automated continuous roll-forming lines punch and profile uprights and beams at controlled thermal conditions with tolerances within ±0.1mm. This eliminates frame twist, ensures upright-to-beam hook connectivity locks without play, and guarantees structural consistency across high-bay installations up to 30 meters.
For standard distribution centers, our electrostatic powder coating provides a 60–80μm durable finish resisting abrasion and humidity. For chemical, outdoor, or sub-zero cold chain deployments, hot-dip galvanization conforming to ISO 1461 is utilized to deliver complete cathodic protection against corrosive elements.
Our engineering team performs localized finite element modeling adhering to Eurocode 8 and ANSI/RMI MH16.1. We factor in local seismic zone acceleration coefficients, calculating baseplate thicknesses, anchor bolt tensile tolerances, and specialized cross-bracing frameworks to ensure absolute stability during seismic activity.
Direct-from-factory certified pallet storage systems, multi-tier platforms, and heavy-duty industrial shelving.
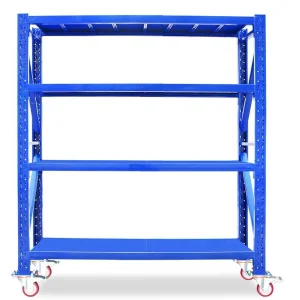
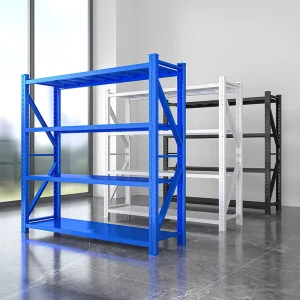
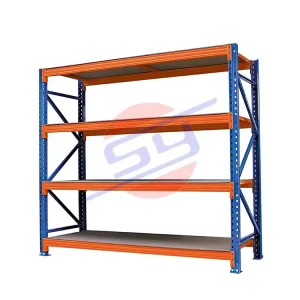
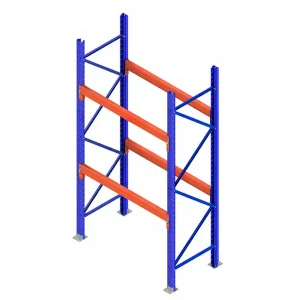
 Sanyang Racking